
Engineering services
The people who engineered it are the people who build it.
PCB, turnkey, box build, harness and cleanroom assembly, backed by an in-house test capability — so a design problem found in manufacturing goes back to the engineers who can change the design.
PCB assembly · Turnkey · Box build · Harness · Cleanroom · Conformal coating
01 — Why the handover costs so much
Most manufacturing problems are design problems.
They just get discovered on the line.
A pad that is hard to place, a connector that cannot be reached, a test point that was never added — each becomes a yield problem, and each has to travel back through an organisational boundary before anyone can fix it.
We build under the same engineering ownership as the design. Design for manufacture is not a gate a supplier applies after the fact; it is a constraint the people drawing the board are already working to, because they will see the first article.
That extends through test. Electrical verification, boundary scan, environmental stress screening and mechanical robustness testing exist to catch what a functional test will not — before a unit ships rather than after it returns.
Talk to Zealogics02 — Where the work happens
Controlled environments, from SMT line to ISO-5.
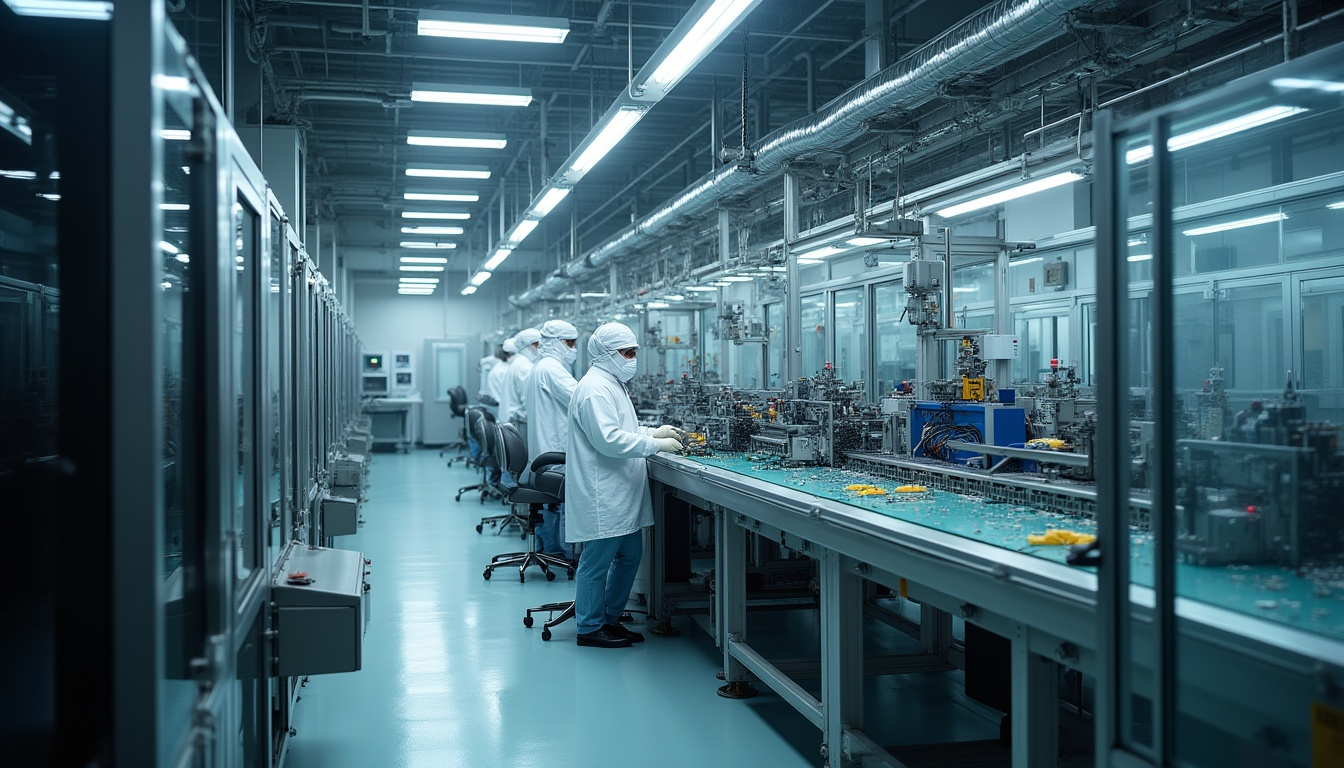
SMT · THROUGH-HOLE · BOX BUILD · CLEANROOM.
03 — What we build
Six build services under one owner.
Test and screening capability
Flying probe test and in-line 3D AOI
JTAG boundary scan test systems
High voltage, insulation and ground bond test
Environmental stress screening and thermal shock
Vibration and bump testing
Solder paste measurement and process control
Standards built to
PCB assembly
Surface mount and through-hole assembly with in-process and functional test, built to CE, UL, RoHS, IPC and ISO requirements.
Turnkey assembly
Design and prototyping, component sourcing, assembly, test and packaging handled end to end, so there is one owner for the schedule and one owner for the yield.
Box build assembly
Simple enclosures through to complex multi-rack systems — mechanical assembly, wiring, integration and system-level test.
Wire and cable harness
High-precision harness manufacturing from design through assembly, built to the exact specification and standards the platform requires.
Cleanroom assembly
Precision electronics and electro-mechanical assembly in controlled ISO-4 and ISO-5 environments, for products where particle contamination is a functional failure.
Mechanical, integrated and additive
High-precision machining and complex electro-mechanical assemblies, integrated manufacturing across disciplines, and additive manufacturing where it shortens development rather than just sounding modern.
04 — What comes with the build
Six things that decide whether volume goes smoothly.
The first article is where a design either proves it can be built repeatably or reveals that it cannot.
01
DFM feedback that reaches the design
Manufacturability findings raised against the drawing while it can still change, not logged as a deviation after the build.
02
First article inspection
A documented first article against the drawing and the BOM, with every deviation dispositioned before the second unit is started.
03
Test coverage plan
Which defects are caught by AOI, which by flying probe, which by boundary scan and which only by functional test — decided rather than assumed.
04
Screening regime
Environmental stress screening, thermal shock, vibration and bump testing matched to how the product will actually be used.
05
Sourcing and BOM control
Component sourcing with qualified alternates and lead-time visibility, so a single part does not stop a build.
06
Build documentation
Work instructions, test records and traceability that survive an audit and a transfer to another line.
05 — How a build runs
Five stages from pack to production.
New product introduction is a stage in its own right here, because that is where the design and the process are reconciled.
Review
Design and manufacturability review of the pack, the BOM and the test strategy.
Source
Component sourcing, alternates qualification and kitting.
Prototype
Prototype build, first article inspection and process development.
Test
Electrical verification, boundary scan, environmental screening and mechanical robustness testing.
Produce
Volume production with documented work instructions, traceability and process monitoring.
06 — Design and build together
A yield problem goes back to the engineer, not to a supplier.
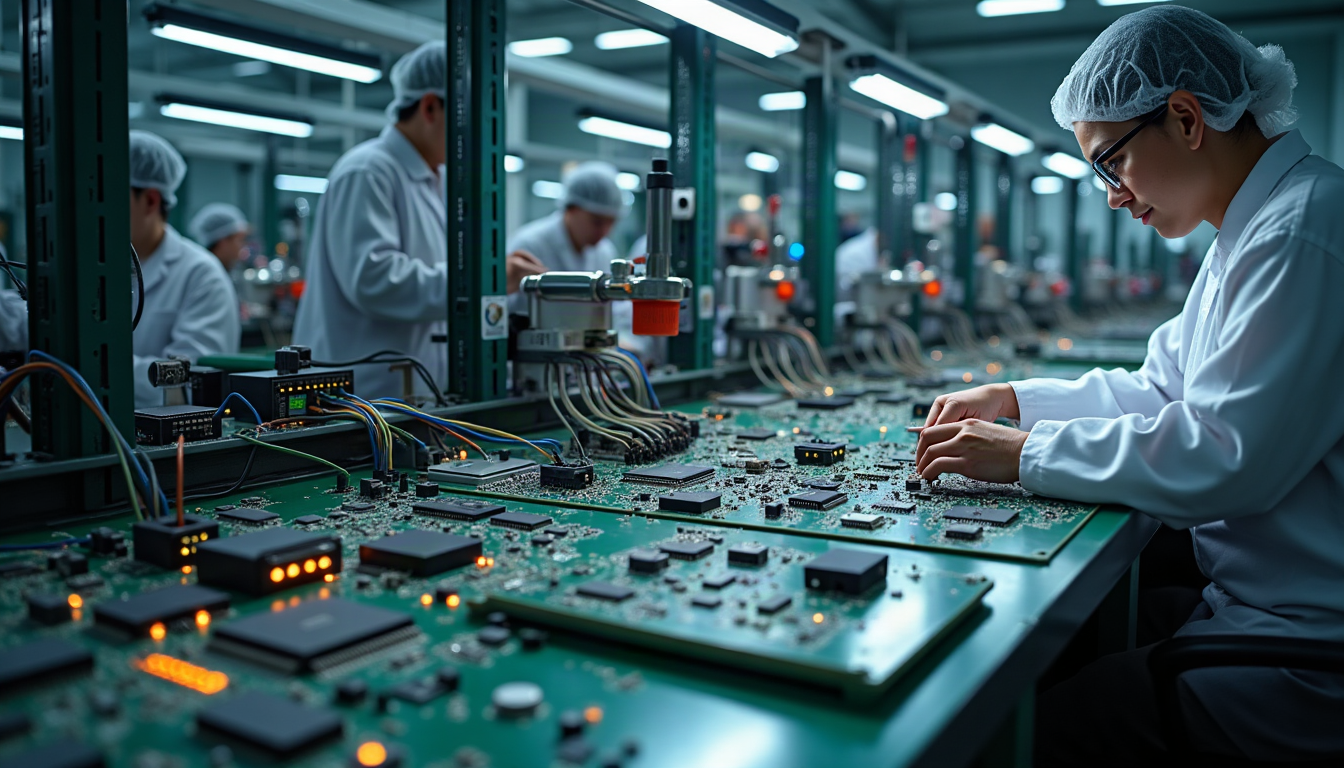
DESIGN · DFM · BUILD · TEST · BACK TO DESIGN.
07 — Sound familiar?
The conversations that start this work.
“Our design house and our builder do not talk to each other.”
Turnkey under one owner
“Yield drops every time we move the board to a new line.”
Process and test transfer
“This assembly cannot be built outside a cleanroom.”
ISO-4 / ISO-5 assembly
“We need low volume now and a route to high volume later.”
NPI and scale-up
“Field failures are not showing up in our functional test.”
Screening and stress testing
“One long-lead component keeps stopping the build.”
Sourcing and BOM control
08 — The rest of the practice
Five more engineering disciplines.
Programmes rarely stay inside one discipline. A tool that needs embedded firmware usually needs the mechanics, the harness and the line that builds it too.
Embed
Embedded Systems
Turn a product concept into hardware and the firmware that runs it — schematics, layout, bring-up, certification and the years of sustenance after.
Explore
Connect
Factory Automation
Equipment software, SECS/GEM and GEM300 integration, EAP and MES connectivity, manufacturing data — and the intelligence layer built on top of them.
Explore
Design
Silicon Engineering
Full-chip design across ASICs, SoCs, FPGAs and chiplets — architecture, RTL, verification, DFT, analog and physical design through tape-out and post-silicon validation.
Explore
Design
Mechanical Engineering
Product design and development, engineering analysis and simulation, model-based systems engineering, and the change management that keeps a design alive for a decade.
Explore
Route
Electrical Engineering
Wiring harness design, 3D routing, schematics, bundling and segregation, power distribution and the build support that gets a harness onto the shop floor.
Explore
Have a problem worth solving?
Send us the pack before you send it to a builder.
A manufacturability and test-coverage review of the design pack usually pays for itself on the first article — and tells you what volume will cost before you commit to it.